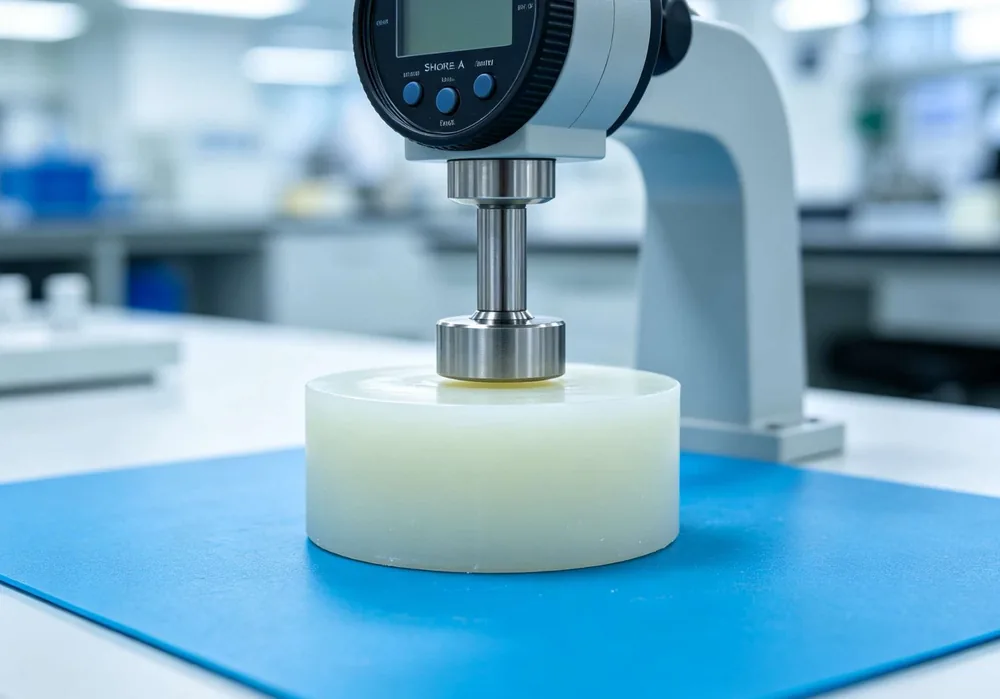
Shore A Hardness
Hardness verified from 20A to 80A against your specification, per batch.
Three-stage quality control — IQC, IPQC and OQC — backed by calibrated measuring equipment and full batch traceability, so every part ships exactly to specification.
Quality is not a final check — it runs through the entire process. Incoming material is verified before use, dimensions are monitored during molding, and every finished batch is inspected before shipping.
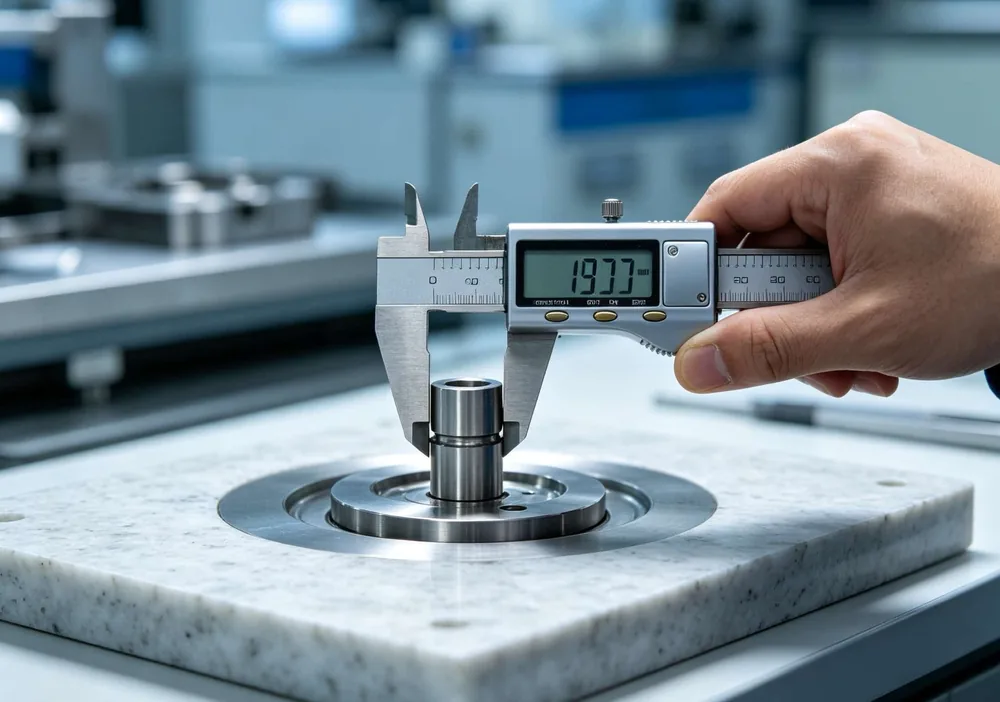
Photographs from our quality lab — the equipment that verifies hardness, tensile strength, dimensions and visual quality on every batch.
Hardness verified from 20A to 80A against your specification, per batch.
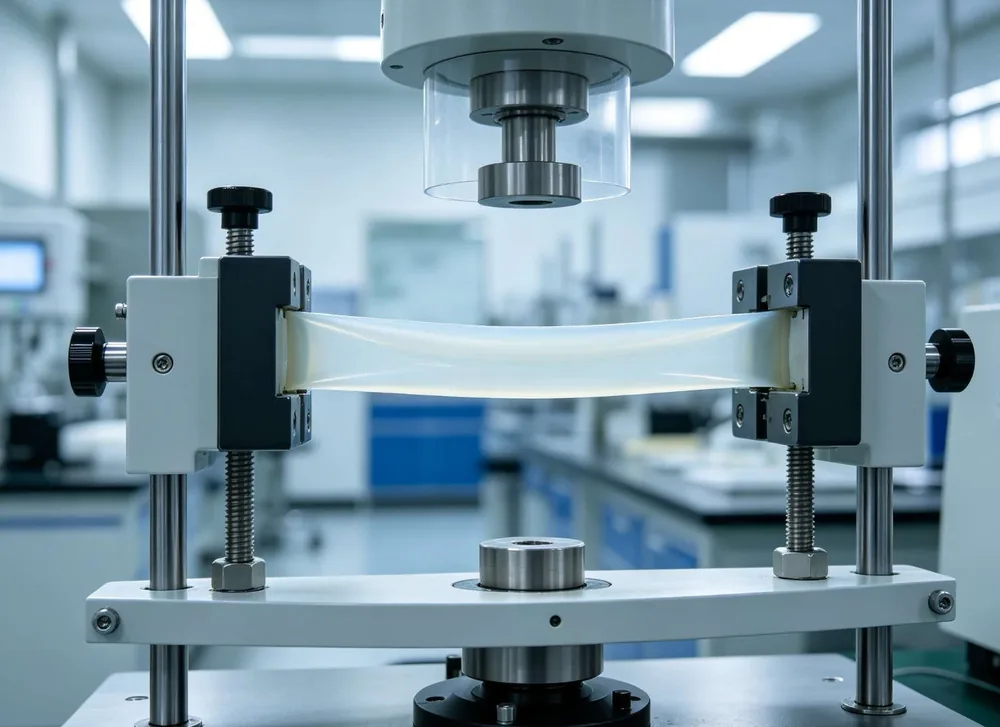
Tensile strength, elongation and tear resistance tested to confirm mechanical performance.
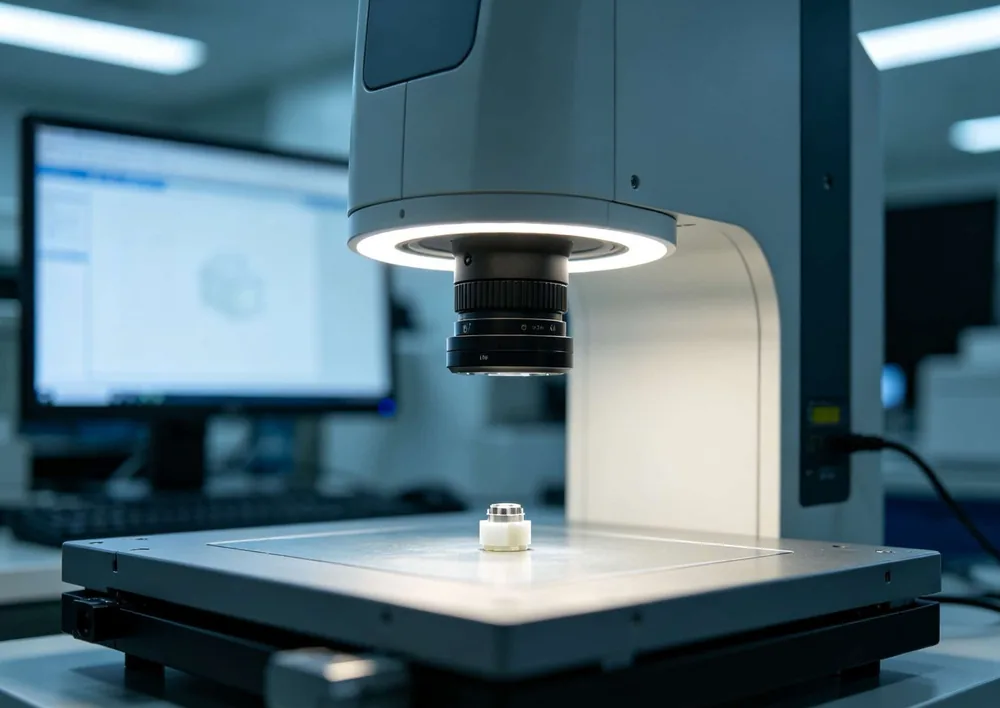
Vision and optical systems measure fine features that calipers cannot reach, and automated optical inspection (AOI) screens surface defects at production speed.
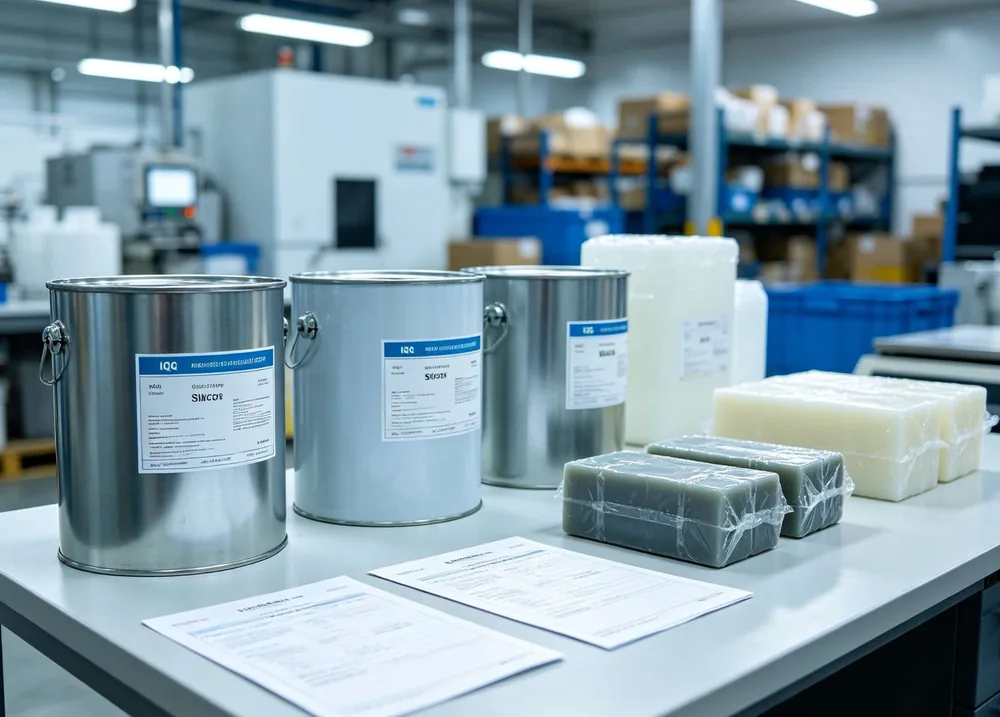
Raw silicone compound checked and certified before it enters production.
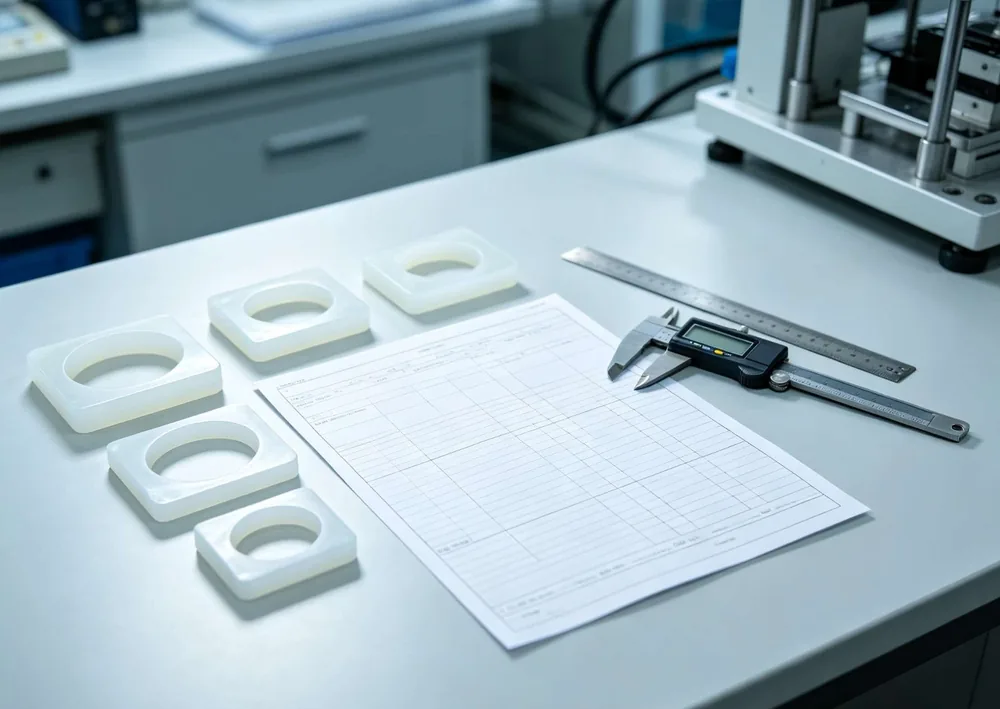
Every batch is documented with dimensional and visual inspection records.
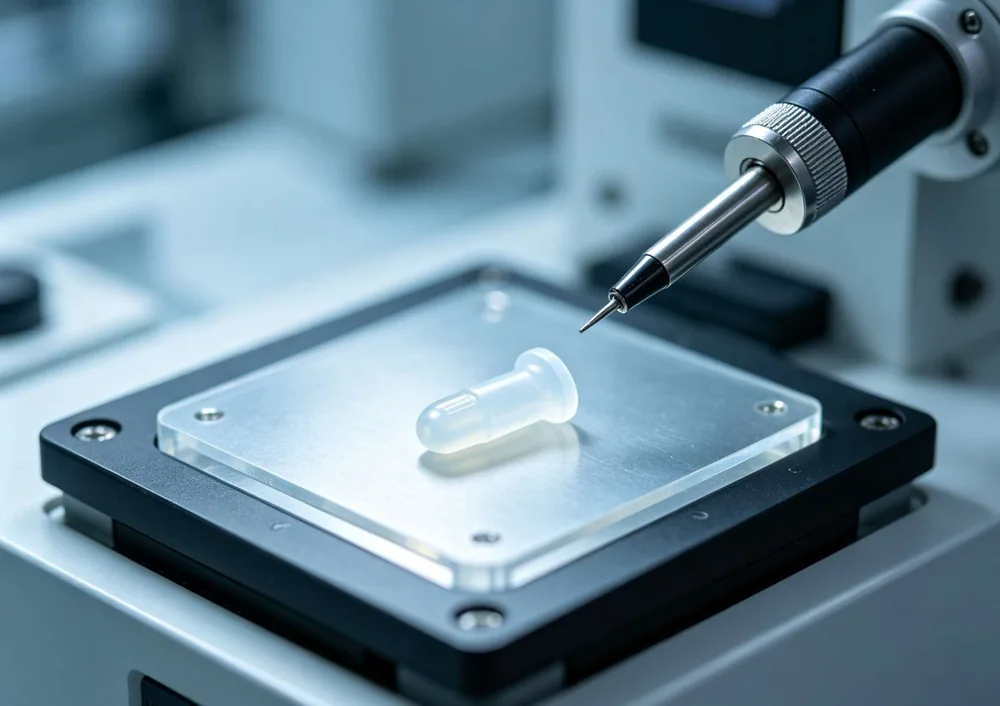
Point-to-point probing verifies critical dimensions on molded components.
Each test method is selected to match your part and market, and the applicable report is supplied with your shipment.
| Test | Method / Scope |
|---|---|
| Hardness | Shore A durometer, 20A–80A |
| Dimensions | Calipers, optical/vision, SPC on critical dimensions |
| Surface & visual | Automated optical inspection (AOI) for defects, flash and contamination |
| Tensile & elongation | Universal tensile tester |
| Color | Pantone match, ΔE ≤ 1.5 |
| Food contact | FDA 21 CFR / LFGB migration testing (where required) |
| Restricted substances | RoHS / REACH screening |
| Traceability | Lot linkage: material → mold → machine → operator |
Critical dimensions are tracked with statistical process control during molding, and every batch is linked back to its raw material, mold, machine and operator — so if a question ever arises, we can trace it to the source.
Process capability is only meaningful when it comes from an actual measured production run. Below is a real SPC study for a medical LSR component — not a headline number, but the result of a documented run.
Characteristic: inner diameter ⌀ 8.00 mm ± 0.02 mm (USL 8.02 mm / LSL 7.98 mm), tracked with X-bar / R control charts.
Pp 1.27 · Ppk 1.19. This measured Cpk reflects the process as it runs today; we monitor it run over run and report the trend, rather than citing a single best case.
The full capability study — control charts, raw measurements and the Cpk calculation — is available on request under NDA for qualified projects.
Note on interpretation: a Cpk of 1.33 is a common general reference, not a universal requirement. The acceptance threshold for any given characteristic is set by your product's specification and the customer's agreed limits — we confirm the applicable Cpk target per part and report the measured result against it, so a figure is never shown out of context.
Tell us your quality requirements and we'll confirm the applicable tests and reports before we start.
Discuss Quality Requirements